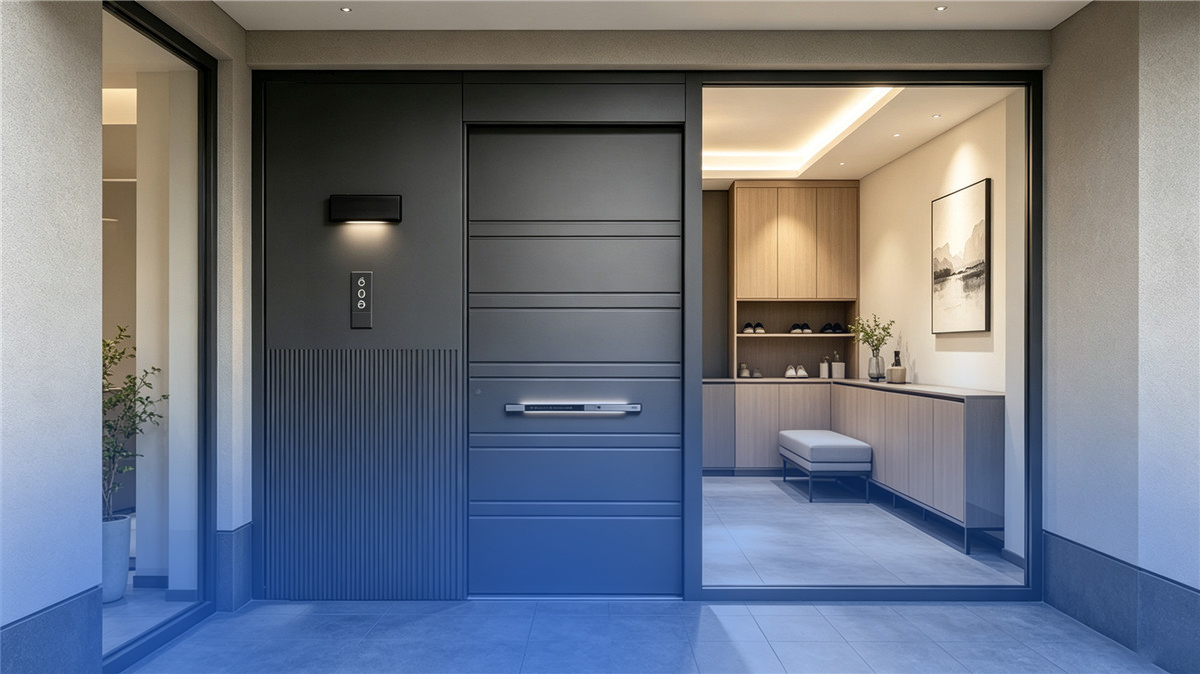
Featured Architectural Entrance Systems
Explore top-tier fenestration units engineered in Foshan, Guangdong. Compliant with international wind loads, thermal efficiency metrics, and seismic safety ratings.
Engineering White Paper: Modern Aluminium Glass Pivot Front Doors
An authoritative technical analysis of mechanical load paths, thermal insulation mechanisms, and fenestration sourcing strategies from China's industrial manufacturing hub.
1. The Kinematics and Structural Topography of Pivot Openings
Architectural design has increasingly moved away from traditional side-hung butt-hinge mechanisms toward large-format pivot front doors. The core mechanical difference lies in how kinetic mass and dead loads are transferred to the building envelope. Traditional side butt hinges create a cantilevered tension-shear load on vertical sub-jambs, which naturally restricts door leaf widths to under 1,100 mm and weights to below 150 kg without risking sag, frame binding, or air-seal degradation.
In contrast, aluminium glass pivot front doors utilize an offset vertical rotational axis situated between 150 mm and 400 mm from the jamb. The entire structural dead load of the oversized sash (frequently exceeding 400 kg to 800 kg in luxury villas and corporate headquarters) transfers vertically into the floor concrete slab via heavy-duty floor springs or precision-machined hydraulic ground boxes. Top pivots operate primarily under horizontal shear load, maintaining sash plumbness across millions of cycles.
2. Material Science: Profile Extrusion & Thermal Barrier Architecture
Chinese fenestration manufacturers lead global supply chains by utilizing aerospace-grade 6063-T6 or 6061-T6 aluminum alloys. Wall thicknesses for structural pivot stiles and rails strictly exceed 2.5 mm to 3.5 mm, ensuring deflection under design wind pressure does not exceed L/175 or L/250 according to ASTM E330 or Australian AS4055 standards.
A critical engineering bottleneck in wide metal doors is the "bimetal effect" (thermal bowing). During peak summer or winter, extreme temperature deltas between indoor climate-controlled spaces and sun-baked exterior surfaces cause differential metal expansion. Advanced Chinese factories mitigate this through split-profile construction joined by glass-fiber reinforced Polyamide (PA66 GF25) thermal barrier strips. These strips mechanically decouple the exterior and interior aluminum skins, curbing thermal conduction (achieving overall assembly U-factors down to 1.4 - 1.8 W/m²·K) while resisting bowing across temperature gradients up to 50°C.
| Engineering Property | Standard Commercial Entry Door | Industrial-Grade Aluminium Glass Pivot Door |
|---|---|---|
| Alloy Specification | 6063-T5 (Wall Thickness 1.4 - 1.8 mm) | 6063-T6 Architectural (Wall Thickness 2.5 - 4.0 mm) |
| Hinge Mechanism | 3 or 4 Surface Butt Hinges / Ball Bearings | Offset Heavy-Duty Hydraulic Ground Pivot (DORMA/FritsJurgens/Custom) |
| Max Leaf Capacity | Width: 1,200 mm | Weight: 120 kg | Width: 2,400 mm+ | Weight: Up to 800 kg |
| Thermal Transmittance (U-Value) | 3.2 - 4.5 W/m²·K (Non-Thermal Break) | 1.2 - 1.8 W/m²·K (Isobaric PA66 Thermal Barrier) |
| Weather Ingress Resistance | Standard Sweep Seal (Prone to friction wear) | Drop-down Mechanical Perimeter Seals + EPDM Vulcanized Gaskets |
3. Air & Water Tightness in Oversized Pivot Fenestration
Historically, the primary operational challenge of pivot doors was weatherproofing. Because the sash rotates along an offset internal axis, standard continuous frame rebates cannot run uninterrupted without impeding bottom clearance. Chinese fenestration engineers solve this via multi-tiered sealing strategies:
First, recessed automatic mechanical drop-down seals are embedded within the base rail. As the door closes into its final 5 degrees of travel, an internal trigger pin contacts the jamb, activating a high-tension spring that plunges an EPDM or silicone neoprene gasket against the finished floor threshold. Second, top and side clearances feature dual-lip vulcanized EPDM gaskets coupled with magnetic threshold contact strips. This multi-plane sealing design enables DERCHI pivot assemblies to pass rigorous wind-driven rain penetration tests (reaching water penetration resistance levels above 450 Pa to 600 Pa under AS2047 and EN 12208 standards).
4. Glazing Specifications for Security and Acoustical Decoupling
The glass unit in a pivot front door serves both aesthetic and physical defense roles. Factory supply specifications demand double- or triple-glazed insulated glass units (IGU). Typical architectural layups incorporate outer lites of 8 mm or 10 mm fully tempered safety glass, an argon gas-filled warm edge spacer (12 mm to 16 mm), and an inner lite of laminated glass (6 mm + 1.52 mm PVB/SGP + 6 mm).
The inclusion of SentryGlas (SGP) interlayers provides blast resistance, hurricane impact resilience, and anti-intruder forced entry delay compliant with European EN 356 Class P5A/P6B. Thermally, Low-E pyrolytic or magnetron sputtering coatings applied to surfaces #2 or #3 achieve Solar Heat Gain Coefficients (SHGC) between 0.22 and 0.35, preventing the greenhouse effect in warm climates without compromising visible light transmission.
Future Procurement Trends in Architectural Doors
Strategic trends transforming global B2B procurement, supply chain logistics, and material integration over the next five years.
Motorized Mechatronics & Smart Access
Commercial and ultra-luxury residential clients now expect complete concealed mechatronics. Procurement specifications increasingly require German or Swiss-engineered motorized locking systems coupled with hidden magnetic sensors, high-speed facial recognition, biometric finger-vein verification, and seamless integration into building automation systems (KNX/Crestron).
Hyper-Customized Material Hybridization
Architects are specifying hybrid composite surfaces. Rather than bare aluminum profiles, front pivots now integrate sintered porcelain slabs, aircraft-grade carbon fiber panels, real stone veneers, cast bronze inlays, and marine-grade thermo-treated wood finishes bonded to thermal-break aluminum chassis via high-modulus polyurethane adhesives.
Carbon Footprint Accountability (EPD)
Global architectural tenders require verified Environmental Product Declarations (EPD). Chinese manufacturing lines are actively shifting toward low-carbon "green aluminum" produced using hydropower or solar energy, cutting cradle-to-gate embodied carbon by up to 60% to meet stringent LEED and BREEAM certification targets.
Enterprise Manufacturing Competencies: Guangdong Dejiyoupin
Operating under the DERCHI brand umbrella, we provide global project developers, builders, and fenestration importers with direct factory accountability.
180,000㎡ Mega Production Infrastructure
Our centralized manufacturing ecosystem in Foshan houses German CNC 5-axis profile machining centers, automated electrostatic powder coating lines, precision glass laminating ovens, and structural silicone assembly bays. This high level of vertical integration prevents multi-tier contractor markups and guarantees rigorous quality control across every door schedule.
Global Standards & Lab Certifications
Our systems undergo extensive physical chamber testing. We maintain active compliance documentation including European CE, ISO 9001 quality systems, Australian AS2047 N6 cyclonic testing, and North American UL fire-rated certifications. Full structural engineering calculations and test reports are provided directly to project consultants for rapid site permit sign-off.
Export Crating & Global Port Delivery
Doors are packed for rigorous sea freight: leaves and frames are sealed in moisture-barrier film, stabilized inside fully-enclosed OSB plywood crates with internal high-density EVA shock absorption, and reinforced with perimeter steel bands. We coordinate consolidated shipping under FOB or CIF terms directly to major ports worldwide (Lagos, Tema, Mombasa, Durban, Sydney, Long Beach, Felixstowe).
BIM & Parametric CAD Shop Drawings
Eliminate site guesswork. Our English-speaking fenestration engineers translate architectural door schedules into fully-annotated CAD shop drawings, connection detail sections, structural anchorage points, and Revit BIM models. Production begins only after strict formal engineering sign-off from your site project team.
Comprehensive After-Sales & Remote Support
Our sales engineering team aligns with global client time zones. In addition to supplying complete installation templates, step-by-step video manuals, and anchor hardware packs, our technical team provides live video support to guide local installation teams during positioning, pivot leveling, and final sealing adjustment.
B2B Sourcing FAQ: Aluminium Glass Pivot Doors
Key technical and contractual answers for architectural contractors, builders, and importers sourcing directly from Chinese manufacturing facilities.